Hidden Costs in Cable & Wire Manufacturing: Where Plants Lose Money
Introduction
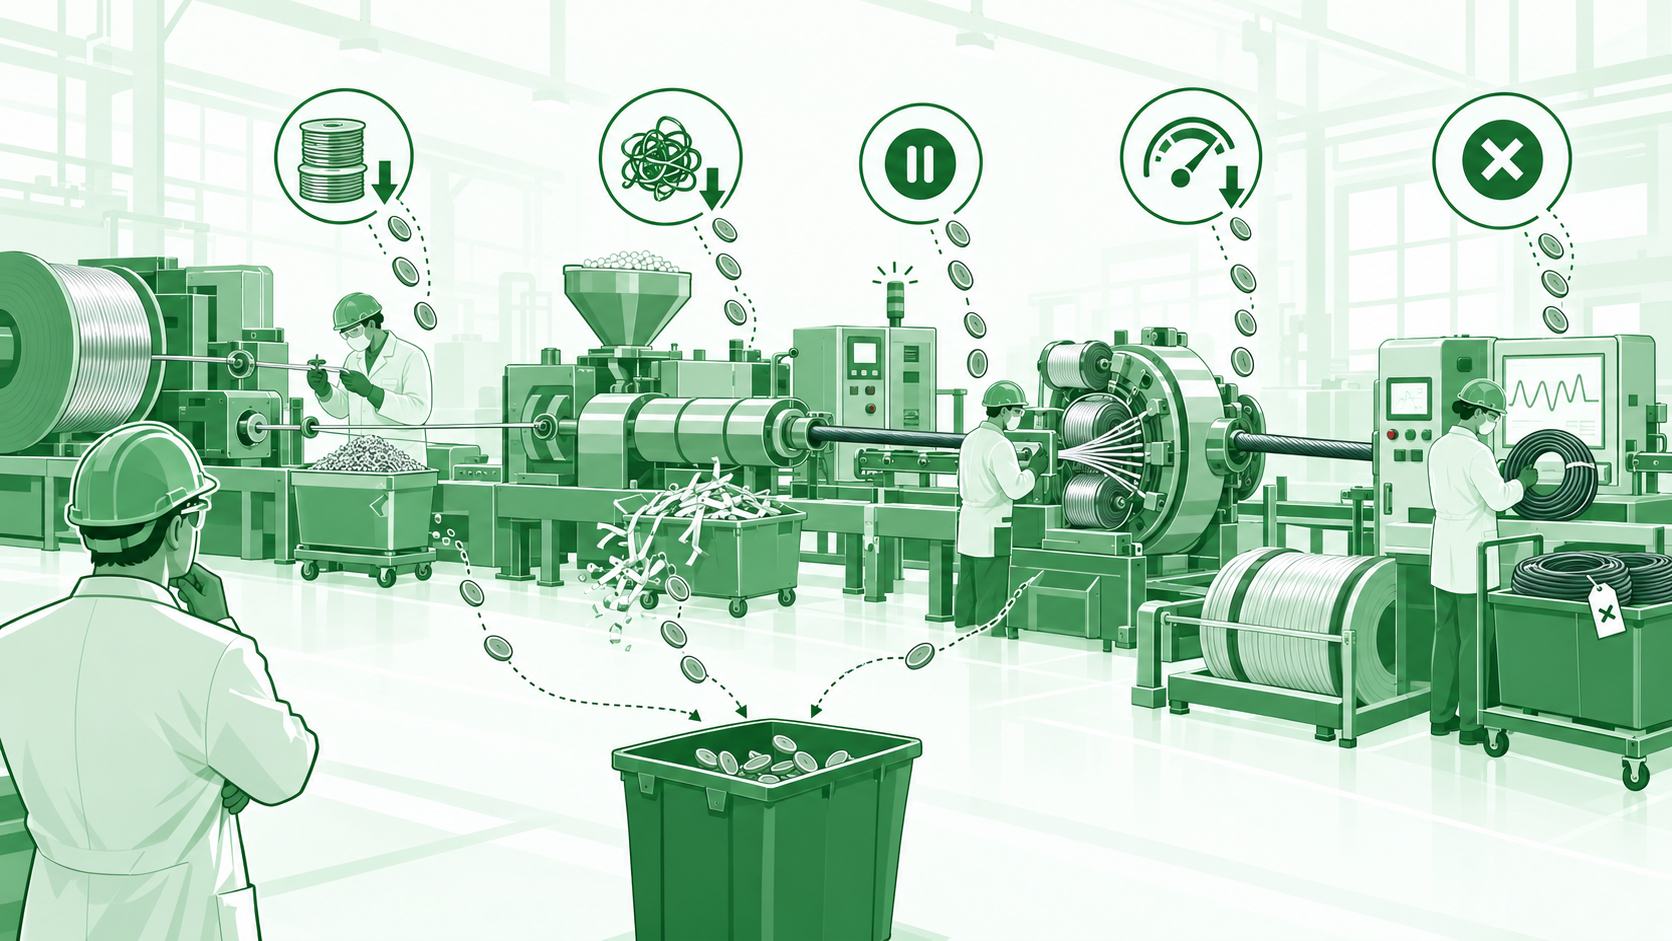
A cable plant can be busy all day and still lose money.
Machines are running, operators are working, and orders are moving, but small losses can add up quickly. Extra copper or aluminium, unplanned scrap, downtime, slow machine speeds, long changeovers, excess inventory and production delays can quietly reduce margins.
The real opportunity is often not adding more machines or people. It is finding where time, material and production capacity are being lost.
Material Waste: A Small Difference Can Become a Big Cost
For cable and wire manufacturers, copper, aluminium, insulation and other materials form a major part of production cost.
During the electric wire manufacturing process and wider cable manufacturing process, material can be lost during setup, cutting, adjustments, defects and rejected production.
A simple check can reveal the difference: planned material use vs. actual material use.
If the numbers do not match, investigate machine settings, product specifications, process conditions, setup practices and material handling.
The goal is not simply to use less material. It is to understand why actual usage differs from the plan.
Scrap and Rework: The Loss May Start Earlier
Scrap is only one part of the larger production loss.
A rejected product may already include material, labour, machine time, electricity and testing costs. Rework adds more processing before the product can be accepted.
The important question is not only "How much scrap did we produce?" It is "Where did the problem begin?" A defect found during final testing may have started much earlier.
Related reading: How to Reduce Scrap in Wire & Cable Manufacturing.
- Incorrect machine settings
- Raw material problems
- Machine condition issues
- Quality failures
- Handling damage
- Process variation
Downtime: When the Machine Should Be Running but Is Not
A machine may be available but still fails to produce what the plan expects.
Breakdowns are one reason. Production can also stop because of material shortages, tool changes, maintenance waiting, operator availability, quality checks or repeated small stoppages.
Do not record only total downtime. Record why the machine stopped.
This helps answer: When the machine was supposed to be producing, what was stopping it?
Speed Loss: The Machine Is Running, but Not Fast Enough
Speed loss is easy to miss because the machine is still producing.
For example, if a machine can realistically produce 100 metres per minute but repeatedly runs at 80 metres per minute, there is no breakdown — but potential output is still being lost.
Track actual production speed against achievable speed for each relevant machine and product.
- Machine condition
- Process instability
- Product characteristics
- Operator settings
- Quality concerns
- Upstream or downstream restrictions
Changeovers Can Quietly Reduce Production Time
Cable plants often produce different sizes, specifications and customer orders. Changing from one product to another may require new tools, dies, materials, machine settings and testing.
Every unnecessary minute during a changeover reduces available production time.
Measure changeover time, setup time, start-up loss, first acceptable output and waiting time.
Then separate work that must happen while the machine is stopped from work that can be prepared beforehand.
The aim is simple: remove unnecessary waiting without rushing the work.
Inventory Can Tie Up Cash Without Improving Production
A warehouse full of material may look safe, but excess stock ties up cash. Too little stock can stop production.
Good cable inventory management means knowing what is available, what is committed, what is moving slowly, what is needed for upcoming orders and which shortages could affect production.
The goal is not a full warehouse. The goal is having the right material when production needs it.
When the Production Plan Does Not Match the Shop Floor
A production plan can look perfect in the morning and change by the afternoon.
A machine may break down. Material may arrive late. An urgent order may come in. A batch may be held because of a quality issue.
When planning and the shop floor use different information, teams make decisions with outdated information.
The result can be: Machine delay → Production delay → Order delay → Dispatch pressure.
Managers need a clear view of what has been produced, what is running, what is waiting and what may be delayed.
Find the Real Bottleneck in the Cable Manufacturing Process
The biggest problem is not always where the delay first appears.
The complete cable production process may look like: Drawing → Stranding → Insulation → Cabling → Sheathing → Testing → Packing → Dispatch.
A restriction at one stage can affect everything that follows.
If drawing cannot supply material fast enough, the next process may wait. If testing becomes the constraint, finished cable may build up before testing.
That is why the complete cable manufacturing process should be reviewed as one connected flow.
- Where is work waiting?
- Why is it waiting?
- How long is it waiting?
- What is causing the restriction?
See the Proof Behind the Approach
Gemba Concepts' cable manufacturing work has focused on practical production issues such as bottlenecks, speed loss, manpower balancing, time-and-motion, SMED and OEE.
One cable manufacturing engagement reported a 53.9% improvement in throughput after addressing production constraints and process performance.
How Gemba Concepts Can Help Cable and Wire Manufacturers
Improvement should start with what is actually happening on the shop floor.
Gemba Concepts uses practical methods such as bottleneck analysis, time-and-motion studies, SMED and OEE to understand where time, material, manpower and machine capacity are being lost.
The approach is simple: See → Understand → Find the Cause → Improve → Measure.
The goal is not to create a report that sits on a desk. It is to identify practical changes that teams can apply and measure.
Where Manufacturing Software Can Help
Technology can make production information easier to see.
Cable manufacturing software, production management software and production tracking software can help teams monitor production status, output, downtime, material usage, quality, orders and machine performance.
Shop floor management software and shop floor control software can bring production information closer to the people managing daily operations.
But software is not the solution by itself.
A dashboard can show where a problem is happening. Process knowledge is still needed to understand why it is happening.
Final Takeaway
Cable manufacturers do not always need more machines or more people.
Sometimes, they need to stop losing the capacity they already have.
Find where material, machine time and production capacity are being lost. Fix the cause, standardize the improvement and measure the result.
Small improvements can make a meaningful difference when the same process runs every day.
Find the Capacity Your Cable Plant Is Already Losing
See where material, machine time and production capacity may be getting lost across your operation.
Written by Mohit Bafna
Co-Founder, Gemba Concepts
- 01
A cable plant can hit its production target and still lose money — the hidden losses sit in material variance, scrap, downtime, speed loss, changeovers, inventory, and planning gaps that repeat every day.
- 02
Speed loss is the easiest loss to miss: a machine that's running but well below its achievable speed shows no breakdown, yet still bleeds capacity.
- 03
The biggest bottleneck isn't always where the delay first appears. Review drawing through dispatch as one connected flow, not isolated stages.
- 04
Software gives visibility into where a loss is happening. Process diagnosis is still needed to explain why.
Frequently asked questions
How to Reduce Scrap in Wire & Cable Manufacturing
The scrap bin tells you how much you lost. It rarely tells you where the loss began — and by the time material reaches it, the copper, aluminium, insulation, and machine time are already gone.
How to Increase Wire & Cable Production Capacity Without Buying New Machines
Before you sign off on a new line, one uncomfortable question — how much of the capacity you already paid for are you quietly throwing away every shift?
How to Reduce Scrap, Material Waste and Rework in Personal Hygiene Manufacturing
Nonwoven trimmings. SAP overshoot. Wet wipes rejected for saturation variance. Every one is material that was paid for, processed, sometimes packed, and then written off.
Industrial Businesses Across 3 Continents